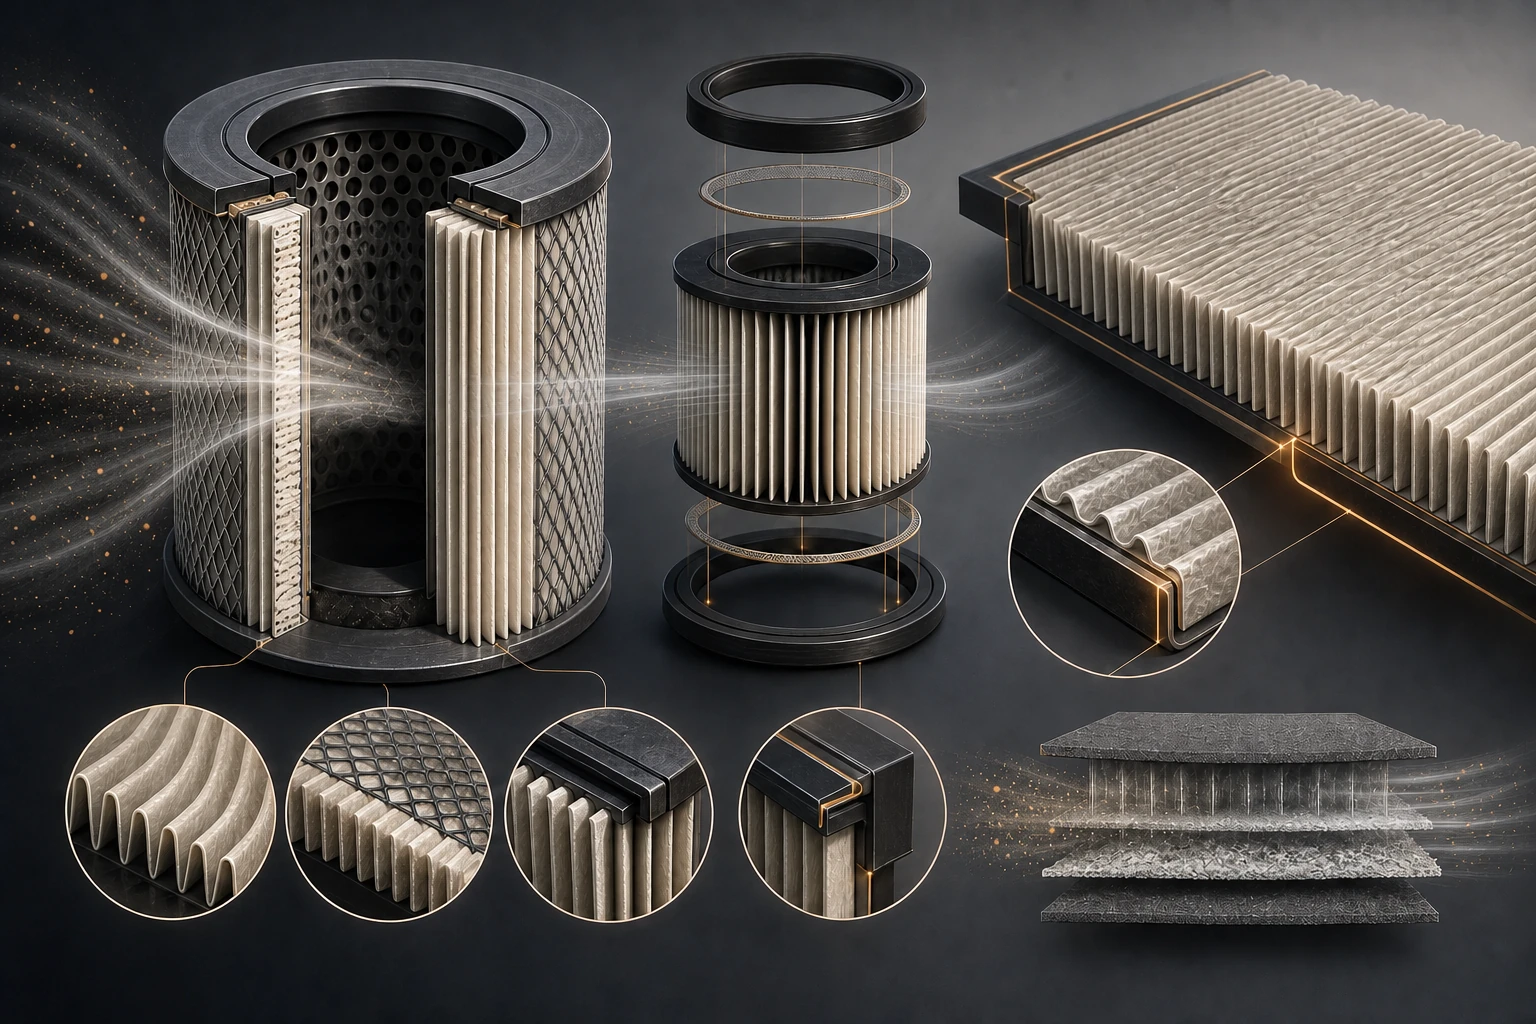
A filter element is defined by performance and construction together. Media selection, pleat geometry, frame stiffness, end sealing, adhesive control and test conditions must work as a single design.
For OEM procurement, product engineering and supplier-quality teams, the strongest sourcing decision comes from linking the part requirement to a practical manufacturing and validation plan. This guide explains what to specify, what to verify and what to include in the RFQ.
The essentials
- Do not buy by outside dimensions alone.
- Tie media and pleat design to airflow and contamination duty.
- Treat seals and bonding as filtration features.
- Compare efficiency and pressure drop only under equivalent tests.
Contaminant, particle size, airflow and media specification
Define the contaminant, particle-size range and operating airflow. Media grade should be controlled by an approved specification and supplier traceability.
Filter media selection and pleat geometry
Pleat height, pitch and count influence area, pressure loss and stability. Pleats need separation and support to prevent bunching or collapse.
Frames, end caps, seals and bonding
Frames must hold geometry without creating installation distortion. End caps and adhesive beads should close every potential bypass path.
What to compare
| Area | Evidence to request |
|---|---|
| Duty | Airflow, contaminant and environment |
| Media | Approved grade and traceability |
| Construction | Pleats, frame, end caps, seals and adhesive |
| Performance | Pressure loss, efficiency and dust-holding method |
| Production | Process checks, sampling and lot records |
Seal compression and adhesive selection
Seal compression needs enough tolerance for both element and housing variation. Adhesive selection should consider media, frame, temperature and fluids.
Adhesive cure control and stated pressure-loss conditions
Cure time and bead continuity require production controls. Pressure loss must be reported at stated airflow and specimen condition.
Efficiency and dust-holding test comparability
Efficiency claims require the challenge aerosol, size range and method. Dust-holding comparisons require the same test procedure and termination rule.
Production checks cannot replace filtration testing
Visual inspection alone cannot confirm filtration performance. Production checks may use dimensions, mass, bonding and approved surrogate tests.
Questions worth asking before nomination
- Which input assumptions could change the tool, process route or quoted price?
- Which characteristics are controlled by process settings, and which require inspection of every part or lot?
- What will be measured during trials, and who approves the result?
- How are material, cavity, machine, assembly and inspection records connected?
- What happens when a drawing, material or demand profile changes after nomination?
Lot traceability should connect media, adhesive, frame parts and test records. The RFQ should include media or performance requirements and the housing interface. These questions turn a capability discussion into a clear technical and commercial responsibility map.
How Premier supports this work
Premier’s available manufacturing scope includes air-cleaner systems and air-filter performance-test equipment. For a filter-element enquiry, buyers should confirm which media converting, pleating, bonding and sealing steps apply to the proposed part.
Premier’s engineering, tooling, manufacturing and quality teams can review the requirement against the drawing, material, production volume and agreed validation plan. The useful starting point is the component data, not a generic capability question.
What to include in the RFQ
- Controlled 3D CAD and the latest drawing revision.
- Component function, mating interfaces and critical characteristics.
- Exact material grade, or the service conditions if material selection is open.
- Annual volume, peak demand, programme timing and target production location.
- Existing tooling status, target machine interfaces and ownership requirements.
- Appearance zones, packaging expectations and traceability requirements.
- Applicable customer specifications, standards and validation methods.
- Samples, mating parts and previous failure information where available.
A complete input pack shortens feasibility review and makes quotations easier to compare. If a value is not yet fixed, identify it as an open engineering decision and provide the condition it must satisfy.
Start a technical review
Send the drawing, material requirement, expected volume and validation plan through Premier’s manufacturing enquiry page. The relevant engineering, tooling, manufacturing and quality teams can then review the part and respond against the actual scope.
Related capabilities
Technical references
- Customer drawing, material specification and applicable validation standards should remain the controlling technical references.