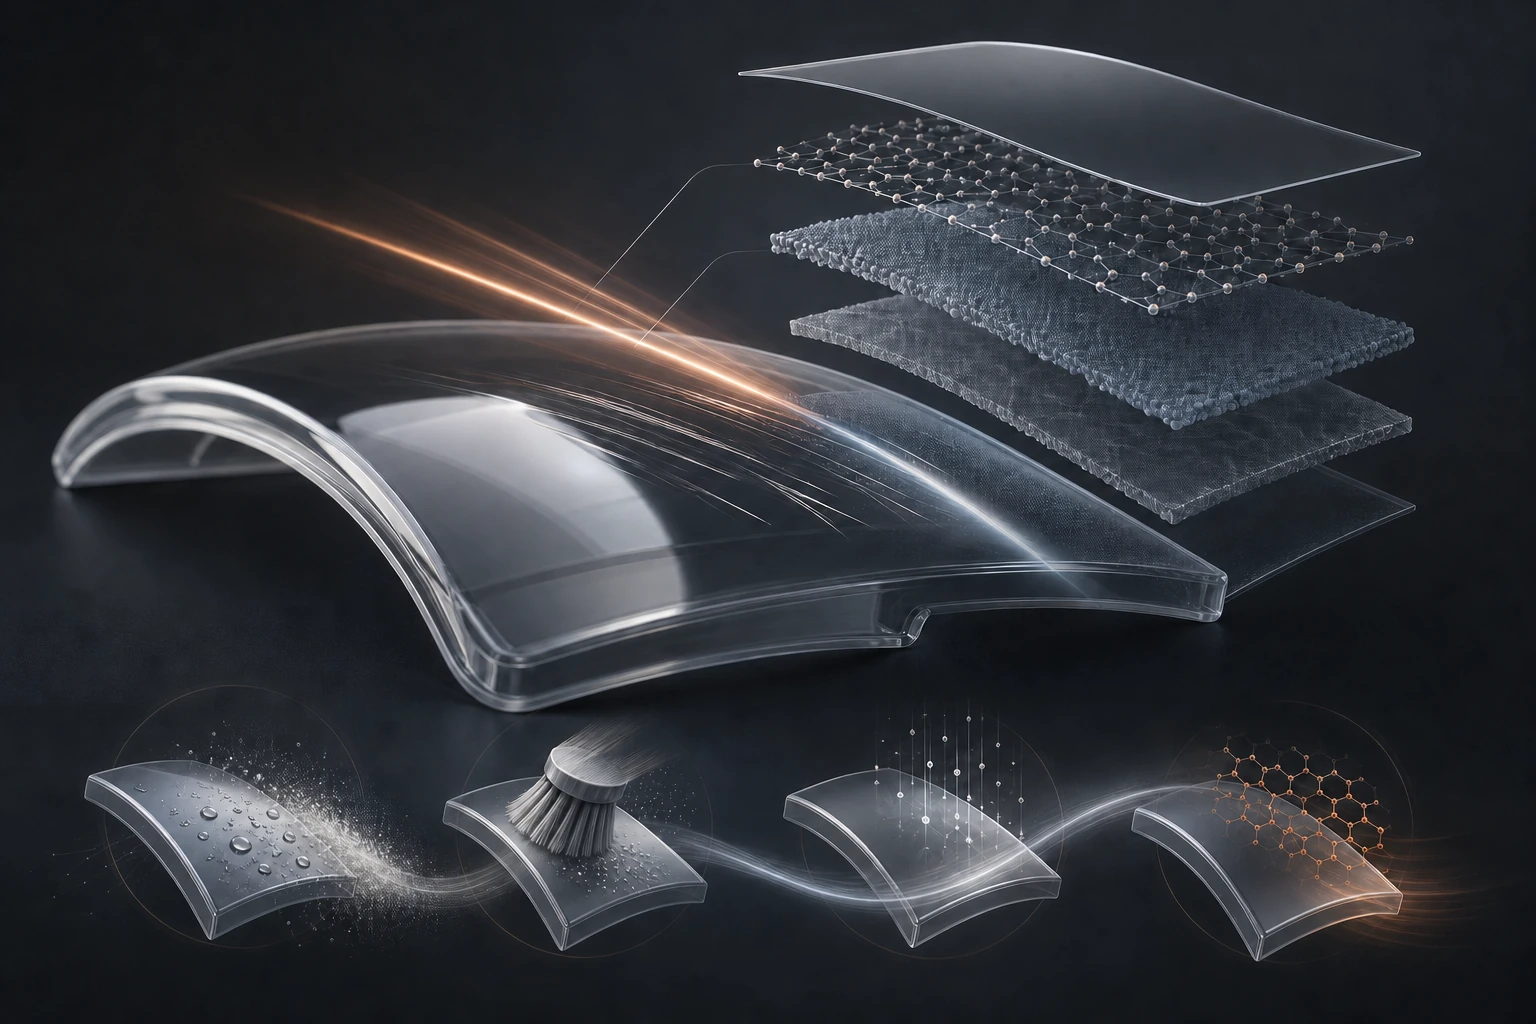
Hard coating is used when an uncoated plastic surface cannot provide the required resistance to scratching, cleaning or environmental exposure. It is not a universal cure: the result depends on substrate condition, coating chemistry, application, cure and handling.
For OEM procurement, product engineering and supplier-quality teams, the strongest sourcing decision comes from linking the part requirement to a practical manufacturing and validation plan. This guide explains what to specify, what to verify and what to include in the RFQ.
The essentials
- Define the failure the coating must prevent.
- Confirm compatibility with the exact substrate and moulded condition.
- Specify test methods and acceptance limits before trials.
- Control cleanliness and handling as tightly as coating application.
Start with substrate condition and service exposure
Start with the uncoated part and the service exposure. Residual moulding stress can affect adhesion, cracking and optical quality.
Additives, contamination and curvature effects
Additives, release agents and contamination may interfere with wetting. Complex curvature can cause film-thickness variation and edge build-up.
Masking boundaries and substrate-safe cleaning
Masked zones and datum surfaces need clear boundaries on the drawing. Cleaning must remove contamination without attacking the substrate.
What to compare
| Area | Evidence to request |
|---|---|
| Substrate | Exact grade, moulding condition and stress limits |
| Surface | Cleaning, masking and contamination controls |
| Coating | Approved system, application and cure route |
| Tests | Abrasion, adhesion, optical and environmental methods |
| Handling | Racking, inspection, protection and rework rules |
Application, cure and visual-defect controls
Application and cure conditions are specific to the selected coating system. Dust, fibres, bubbles, runs and orange peel need visual standards.
Defined abrasion and adhesion test methods
Abrasion resistance must cite the instrument, load, wheel or medium and cycle count. Adhesion testing requires a named method and conditioning state.
Optical and environmental test requirements
Optical parts may need haze, transmission and distortion measurements. Environmental tests should reflect temperature, humidity, chemicals and cleaning agents.
Measured performance and damage-free handling
A cosmetic pass does not replace measured performance evidence. Protected racks, gloves and inter-operation packaging reduce handling damage.
Questions worth asking before nomination
- Which input assumptions could change the tool, process route or quoted price?
- Which characteristics are controlled by process settings, and which require inspection of every part or lot?
- What will be measured during trials, and who approves the result?
- How are material, cavity, machine, assembly and inspection records connected?
- What happens when a drawing, material or demand profile changes after nomination?
Rework rules should state whether stripping is allowed and how the substrate is protected. The RFQ should include substrate, zones, test methods, appearance limits and volume. These questions turn a capability discussion into a clear technical and commercial responsibility map.
How Premier supports this work
Premier can review the moulded-part geometry, substrate, finish zones and validation requirements as part of a component enquiry. The exact coating process, equipment and test scope should be confirmed against the submitted specification.
Premier’s engineering, tooling, manufacturing and quality teams can review the requirement against the drawing, material, production volume and agreed validation plan. The useful starting point is the component data, not a generic capability question.
What to include in the RFQ
- Controlled 3D CAD and the latest drawing revision.
- Component function, mating interfaces and critical characteristics.
- Exact material grade, or the service conditions if material selection is open.
- Annual volume, peak demand, programme timing and target production location.
- Existing tooling status, target machine interfaces and ownership requirements.
- Appearance zones, packaging expectations and traceability requirements.
- Applicable customer specifications, standards and validation methods.
- Samples, mating parts and previous failure information where available.
A complete input pack shortens feasibility review and makes quotations easier to compare. If a value is not yet fixed, identify it as an open engineering decision and provide the condition it must satisfy.
Start a technical review
Send the drawing, material requirement, expected volume and validation plan through Premier’s manufacturing enquiry page. The relevant engineering, tooling, manufacturing and quality teams can then review the part and respond against the actual scope.
Related capabilities
Technical references
- Customer drawing, material specification and applicable validation standards should remain the controlling technical references.