Injection Moulding
Precision across a broad moulding range.
Injection moulding supports small precision parts, large-format components, co-moulded assemblies and controlled-surface applications.
What we can support
Process range, production control and assembly-ready output.
Equipment configuration and process control are selected around component geometry, material and downstream requirements.

Range
Moulding configurations
Conventional injection, twin-shot moulding, vertical barrels and rotating platens support diverse component architectures.
Review manufacturing
Control
Repeatable production
Centralised material conveying, robotic handling and process controls support repeatable output.
Review infrastructure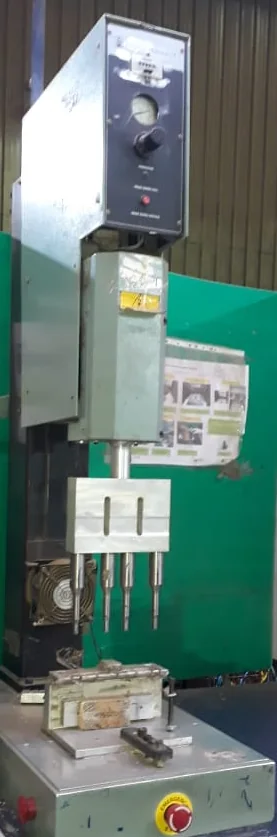
Completion
Assembly-ready parts
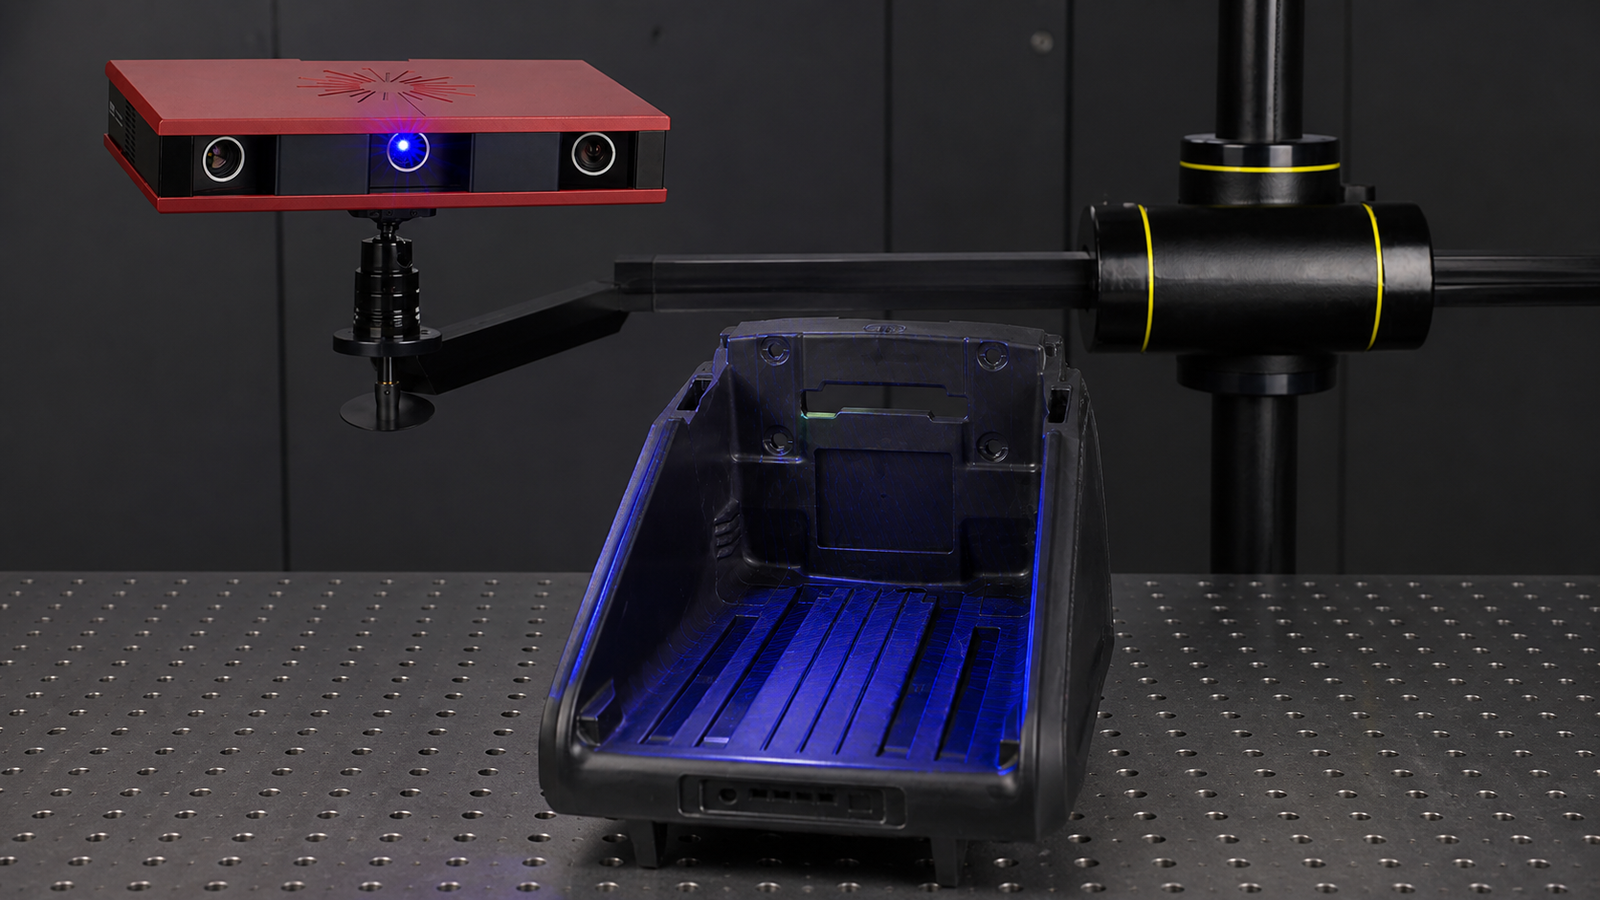
Threads, weld interfaces, cosmetic surfaces and pressure-critical features are developed for downstream operations.
Review completionHow the work moves
The moulding route is controlled from requirement to release.
- 01
Geometry and functional requirements establish the injection-moulding brief. Programme inputs
Confirm component geometry, resin, finish, volume and critical characteristics.
Review engineering - 02
Tool readiness
Review the mould, cooling strategy, interfaces and trial status before production.
Review tooling - 03
Controlled material movement precedes the moulding cycle. Material control
Define resin handling, preparation, conveying and traceability requirements.
- 04
The process window is established around the component and tool requirement. Process setup
Establish the equipment configuration, process window and in-process controls.
- 05
Controlled production
Run the approved process with robotic handling and defined inspection checks.
Review manufacturing - 06
Joining and release evidence complete the injection-moulding route. Completion and release
Complete downstream operations and review dimensional or functional evidence.
Review completion
Discuss your requirements
What the engineering team reviews at each gate.
| Stage | Review focus | Expected output |
|---|---|---|
| Programme input | Geometry, resin, finish, volume and critical characteristics | Approved input brief |
| Tool readiness | Mould, cooling, interfaces and trial status | Trial-ready tool |
| Process control | Material handling, equipment configuration and process window | Controlled production route |
| Completion and release | Joining plus dimensional or functional checks | Release evidence |
Talk to our team
Discuss the requirement in context.
Begin with the application, material, tooling status, validation needs and programme timing.